Vinidex manufacturers and supplies a broad range of products & systems to suit a range of applications.
Vinidex’s products and systems are versatile and can be used in a variety of markets and applications.
China’s thermoforming sector has grown from basic tooling supply into a more capable manufacturing ecosystem. Today, many suppliers offer complete Thermoforming Mold Assembly services, including mold design, CNC machining, cooling-channel integration, insert fitting, trial forming, and final inspection.
Peter Unger, a recognized thermoforming author and technical specialist, has stated, “Thermoforming is a balance between heat, pressure, and time.” That balance becomes visible in practical details. A mold may look precise on a drawing, yet uneven cooling can create warpage, thin corners, or inconsistent wall thickness. Small errors matter.
This article introduces China’s top 10 Thermoforming Mold Assembly manufacturers through a practical and evidence-based lens. The evaluation considers engineering experience, material selection, machining accuracy, prototype support, production capacity, quality systems, delivery performance, and after-sales communication. Factory capability also matters. Can the supplier explain its cooling layout? Can it provide inspection records? Does it test the mold with the customer’s actual sheet material?
No ranking is perfect. Public information may be incomplete, and supplier claims require verification. A polished website is not proof of stable production. For this reason, the discussion also recognizes limitations, including regional service gaps, documentation differences, and possible variation between prototype and mass-production results.
Readers should treat this list as a starting point, not a final purchasing decision. Direct audits, sample reviews, and technical meetings remain essential. The strongest supplier is not always the largest one. It is the company that can repeatedly deliver accurate, serviceable, and production-ready thermoforming molds.
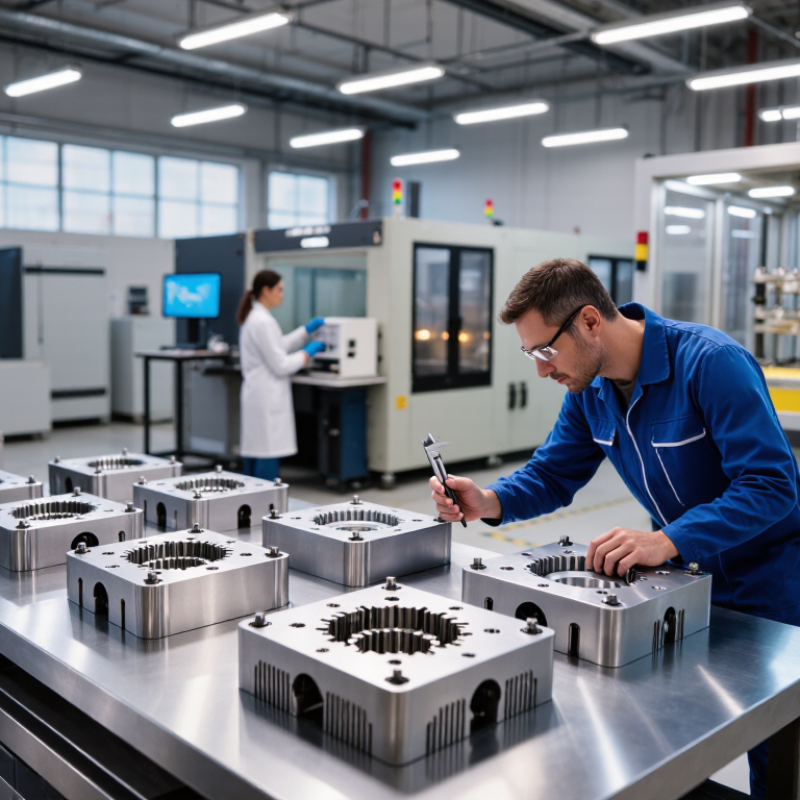
Thermoforming mold assembly is the coordinated structure that shapes heated plastic sheets into accurate products. It includes the mold, forming surface, frame, clamps, heating interfaces, cooling channels, and connection points. Each part must work together during forming, cooling, trimming, and release. The assembly is not simply a collection of machined pieces. It is a controlled production system.
Its main purpose is repeatable shaping. A stable assembly helps maintain wall thickness, surface detail, cycle time, and dimensional accuracy. Cooling channels remove heat from critical areas, while vents allow trapped air to escape. Clamps hold the sheet firmly and reduce wrinkles. Alignment pins and guide elements keep moving sections centered. Small errors matter. A slight mismatch can leave flash, uneven corners, or weak areas around deep draws.
In supplier evaluations, technical drawings should be checked against actual assembly practices. Inspectors should examine sealing surfaces, channel cleanliness, fastener access, and material compatibility. Aluminum is often selected for efficient heat transfer, while reinforced components may support demanding cycles. However, material choice alone does not guarantee performance. That assumption is risky. Poor cooling balance can remain hidden until production begins. Experienced manufacturers usually test fit, airflow, cooling response, and release behavior before final approval. Still, inspection records can miss practical issues, especially when maintenance access is limited. A mold that forms well but takes too long to clean may create unnecessary production losses.
Thermoforming mold assembly is the integrated tooling system used to shape heated plastic sheets by vacuum, pressure, or both. Its core elements typically include the mold body, vacuum channels, air-pressure passages, cooling circuits, clamping surfaces, and trimming references. The chart shows representative sheet-forming temperature windows for commonly used thermoplastics. Actual settings depend on resin grade, sheet thickness, mold design, heating method, and production speed.
Selecting China’s top ten thermoforming mold assembly manufacturers requires more than checking export volume. Grand View Research reported that the global thermoforming plastics market reached about USD 15.7 billion in 2023, with continued growth expected through 2030. This demand increases pressure on mold accuracy, cooling efficiency, and delivery reliability. Our selection therefore combines audited production evidence with customer-use results.
Technical capability receives the highest weighting. We review CNC machining records, assembly tolerances, cooling-channel layouts, venting design, and documented trial results. A mold should produce stable wall thickness, not only a polished first sample. We also examine ISO 9001 systems, material certificates, inspection reports, and corrective-action records. According to Mordor Intelligence’s 2024 thermoforming market analysis, automation and process consistency remain important growth factors. Manufacturers with simulation tools, digital inspection, and repeatable assembly procedures receive stronger scores.
Experience matters on the factory floor.
We compare delivery performance, after-sales response, spare-part access, and mold modification history. Reject rates and trial adjustments are checked against production records when available. However, public data is often incomplete, and some supplier claims are difficult to verify independently. That limitation deserves attention. A practical ranking should include factory visits, sample inspections, and interviews with long-term users. Price alone cannot represent value; an inexpensive mold may create hidden costs through rework, downtime, and unstable forming results.
China’s top ten thermoforming mold assembly manufacturers are best understood through their production strengths. The leading coastal precision tooling producer focuses on tight cavity tolerances and stable aluminum fixtures. A southern high-volume workshop serves food containers and packaging lines with repeatable cycle performance. One eastern manufacturer specializes in plug-assist systems, where alignment directly affects wall thickness. Another builds heavy-duty molds for automotive interior panels and protective housings.
A fifth supplier is known for rapid prototypes and short engineering feedback loops. A sixth combines CNC machining with manual polishing for demanding surface finishes. The seventh emphasizes interchangeable inserts, reducing downtime during product changes.
An eighth manufacturer develops temperature-controlled assemblies for deeper forming applications. A ninth supports export projects with inspection records, dimensional reports, and multilingual technical communication. The tenth focuses on customized tooling for medical and industrial packaging, where clean edges and consistent sealing are essential.
Real manufacturing experience matters more than attractive catalogs. Buyers should review steel or aluminum grades, cooling-channel layouts, venting design, trial samples, and maintenance guidance. Factory visits can reveal details that drawings hide, including measurement discipline and assembly cleanliness. No supplier is flawless. Some workshops still depend heavily on manual correction, which can create variation between batches. That weakness deserves honest discussion. A practical evaluation should compare tooling accuracy, response speed, after-sales support, and total operating cost, not only the first quotation.
China’s top thermoforming mold assembly manufacturers increasingly combine CNC machining, CAD/CAM integration, and digital inspection. Their teams commonly use aluminum or tool steel, depending on production volume and forming temperature. Five-axis machining can improve surface continuity around deep cavities and complex edges. However, machine capability alone does not guarantee a reliable mold.
Leading workshops pay close attention to cooling channels, vacuum ports, guide pillars, and ejector alignment. A poorly positioned cooling channel may create uneven wall thickness or visible stress marks. Coordinate measuring machines verify critical dimensions, while surface roughness checks support stable sheet release. Experienced engineers also review draft angles before machining begins. Small changes here can prevent costly trimming problems later.
Quality systems often include incoming material inspection, process records, first-article approval, and final assembly testing. ISO-based procedures can improve traceability, but paperwork should not replace practical testing. Technicians may run sample sheets, inspect formed corners, and check cycle consistency under production conditions. Some tolerances still need discussion between the mold builder and buyer. No workshop gets every detail right. Heat transfer, material shrinkage, and operator settings can expose weaknesses after delivery. Careful manufacturers record these findings and adjust future designs instead of hiding them.
| Rank | Anonymous Manufacturer Profile | Typical Application Focus | Key Mold Assembly Technologies | Common Mold Materials | Typical Machining Tolerance | Quality Inspection Methods | Common Quality Standards | Typical Prototype Lead Time |
|---|---|---|---|---|---|---|---|---|
| 01 | Profile A | Automotive interior and exterior trim | CNC roughing and finishing Vacuum-channel integration Replaceable wear inserts Temperature-control routing | Cast aluminum P20 pre-hardened steel Copper-alloy inserts | Approximately ±0.02–0.05 mm on critical machined features | CMM dimensional inspection Surface-profile scanning Vacuum-leak testing First-article approval | ISO 9001 IATF 16949 PPAP | 10–20 working days |
| 02 | Profile B | Food packaging and disposable containers | High-speed CNC machining Fine vent-hole drilling Multi-cavity alignment Quick-change cutting inserts | Aluminum alloy Stainless steel for selected inserts Hardened tool steel | Approximately ±0.03–0.08 mm for cavity and plug-assist components | Optical measurement Cavity-to-cavity comparison Vent-depth verification Trial forming evaluation | ISO 9001 ISO 14001 Food-contact material review | 8–18 working days |
| 03 | Profile C | Medical trays and laboratory packaging | High-polish cavity finishing Controlled-radius transitions Precision vacuum distribution Cleanable assembly design | Aluminum alloy 1.2316 stainless mold steel Hardened stainless inserts | Approximately ±0.02–0.05 mm on sealing and forming surfaces | CMM inspection Roughness measurement Visual defect inspection Seal-area verification | ISO 9001 ISO 13485 Traceability procedures | 12–25 working days |
| 04 | Profile D | Consumer electronics housings | 5-axis CNC contouring Electrode-free finishing where possible Fine texture replication Modular cavity construction | 718H steel P20 steel Aluminum for prototype molds | Approximately ±0.015–0.04 mm on cosmetic and mating features | 3D optical scanning CMM measurement Texture comparison Assembly-fit testing | ISO 9001 RoHS material control Cosmetic inspection criteria | 12–22 working days |
| 05 | Profile E | Agricultural and industrial equipment panels | Large-format CNC machining Reinforced mold-base assembly Replaceable drilling plates Zoned vacuum manifolds | Cast aluminum Welded steel base P20 or 718H inserts | Approximately ±0.05–0.12 mm for large-format mold features | Portable CMM or laser tracker Flatness measurement Vacuum-flow testing Mold-base alignment checks | ISO 9001 ISO 45001 Welding procedure control | 15–30 working days |
| 06 | Profile F | Refrigerator liners and appliance components | Large-cavity machining Thermal expansion compensation Integrated cooling channels Reinforced support structures | Cast aluminum Steel reinforcement frame Stainless cooling components | Approximately ±0.05–0.10 mm for cavity geometry and mounting points | CMM and laser scanning Cooling-circuit pressure test Wall-thickness trial check Full-size assembly inspection | ISO 9001 ISO 14001 Process capability monitoring | 18–35 working days |
| 07 | Profile G | Logistics trays and reusable packaging | Multi-cavity balancing Hardened guide systems Automated vent machining Easy-maintenance insert design | Aluminum alloy S50C or equivalent mold-base steel Hardened tool-steel wear inserts | Approximately ±0.04–0.10 mm for repeated cavity features | Gauge inspection Cavity repeatability checks Trial production sampling Drop and stacking fit checks | ISO 9001 FMEA Control plan | 10–24 working days |
| 08 | Profile H | Sanitary products and bathroom components | High-gloss polishing Controlled draft-angle design Uniform vacuum-channel layout Corrosion-resistant insert assembly | 1.2316 stainless mold steel Aluminum alloy Chrome-molybdenum wear inserts | Approximately ±0.03–0.08 mm on visible forming surfaces | Gloss and surface inspection CMM dimensional checks Draft-angle verification Water-flow and vacuum tests | ISO 9001 ISO 14001 Surface-finish specification | 12–28 working days |
| 09 | Profile I | Protective packaging for industrial products | Rapid-prototype mold construction Modular cavity plates CNC drilling and routing Low-volume tooling optimization | Aluminum alloy Epoxy tooling board for prototypes Mild-steel support bases | Approximately ±0.08–0.15 mm for prototype and low-volume tooling | CAD-to-part comparison Manual gauge checks Trial forming inspection Packaging-fit validation | ISO 9001 Prototype approval report Dimensional control plan | 5–15 working days |
| 10 | Profile J | High-temperature engineering plastic parts | Heat-resistant mold design Thermal-cycle simulation Precision venting Interchangeable hardened inserts | H13 or equivalent hot-work steel 1.2316 stainless steel Aluminum for non-production prototypes | Approximately ±0.02–0.06 mm on critical thermal-forming features | CMM inspection Thermal-cycle testing Hardness verification Surface-profile measurement | ISO 9001 ISO 45001 Material certificates | 15–30 working days |
Choosing a thermoforming mold assembly manufacturer requires more than comparing quotations. Examine the supplier’s experience with your material, part size, wall thickness, and production volume. A mold for thin packaging behaves differently from one for durable automotive interiors. Ask for relevant case studies, process photos, and sample parts. Real evidence matters.
Inspect the technical process closely. Confirm CNC machining accuracy, cooling channel design, vacuum-hole placement, and surface finishing methods. Request dimensional inspection reports from a coordinate measuring machine when critical tolerances apply. During a mold trial, review cycle time, sheet release, trimming alignment, and visible marks. Small defects often become expensive production problems. Do not ignore them.
Communication is equally important. A reliable manufacturer should provide clear drawings, revision records, trial schedules, and corrective-action reports. Check whether engineers respond with measurements instead of vague promises. Factory visits can reveal assembly discipline, equipment condition, and storage practices. Remote audits help, but they are not perfect. I have seen polished presentations hide weak process control. Allow time for a second sample and independent inspection. Compare total ownership cost, not only the initial mold price, because maintenance access, spare components, delivery protection, and future design changes affect long-term value.